Synchronize the evidence
Use one clock basis for controllers, counters, utility trends and manual observations. Validate that running, starved, blocked and fault states represent the physical condition during a planned check.
Production Performance Brief
Find the initiating loss before replacing equipment. A stopped filler can be a downstream symptom of a packer interruption rather than the source of the problem.
Direct answer
Review point 01
An empty infeed directs the check upstream. A full discharge directs it downstream. Normal movement with low accepted counts directs it toward rejection, holds or count reconciliation. None of these observations alone proves that a particular machine needs replacing.
Review point 02
Example only: at 10:14:00 the packer stops for film replenishment; at 10:14:20 downstream accumulation fills; at 10:14:25 the filler reports blocked; at 10:15:10 the packer restarts; at 10:15:35 the filler resumes. The 70-second filler stop is a propagated loss. The packer event plus buffer and recovery behavior deserve investigation first.
Review point 03
Choose a representative production window with one SKU and record good output, rejects, machine states and material events. Preserve unknown causes instead of forcing them into a convenient category. If logging is manual, use a shared clock and capture the first observed event.
Review point 04
Compare maintenance or material recovery, replenishment practice, control changes, usable accumulation and capacity replacement against the same baseline. Qualified personnel must follow the equipment safety procedures; never bypass guards, emergency stops or interlocks to keep the line running.
Catalog equipment evidence
These Allot Tech catalog references connect the technical explanation to physical equipment. Each caption identifies the capacity, interface or acceptance evidence to confirm.
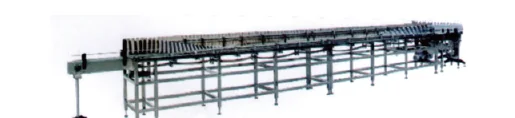
Usable accumulation is a controlled time buffer, not simply conveyor length. Confirm bottle stability and recovery after stops.
Review this interface basis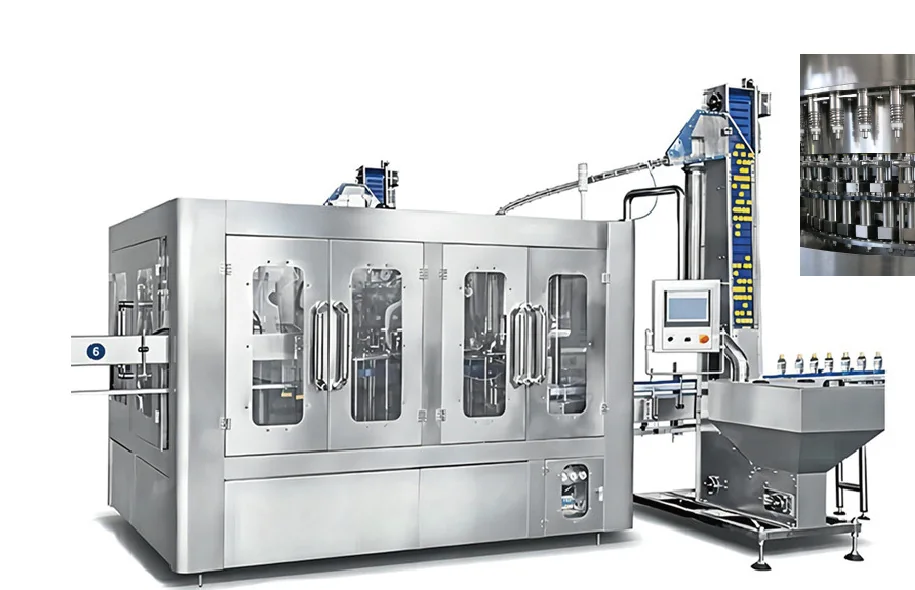
State filler BPH with the reference bottle, product, cap, test window and accepted-output counting point.
Review this interface basis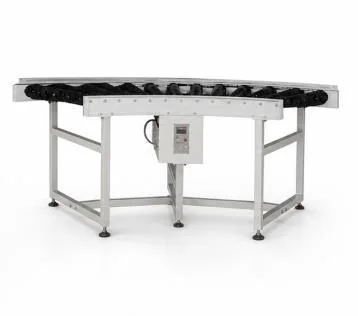
Transfer plates, guides, elevations and speed zones must suit the approved bottle under real wet and dry conditions.
Review this interface basis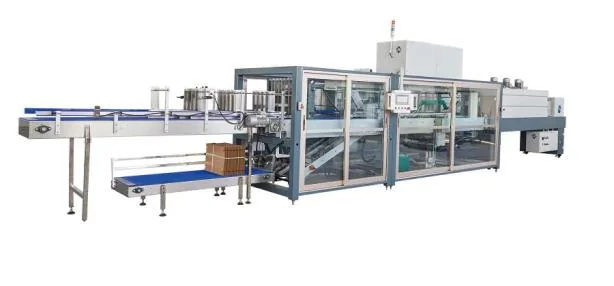
The packer is one connected capacity node; pack pattern, cycle, bottle behavior and discharge flow set the usable rate.
Review this interface basisSource: Allot Tech Beverage Bottling Catalog 2026. Images are representative equipment references; final models and configurations remain project-specific.
Event-chain diagnosis
The machine that stops visibly is often reporting a condition created elsewhere. A defensible bottleneck review aligns equipment states, buffer occupancy and good-output counts on one timeline before choosing a corrective action.
Use one clock basis for controllers, counters, utility trends and manual observations. Validate that running, starved, blocked and fault states represent the physical condition during a planned check.
Identify which state changed first, how full or empty buffers propagated the event, which machines were affected and when good output returned to the pre-event basis.
After a correction, repeat the same representative run. Confirm that sustained good output improved and that the loss was not transferred to labeling, packing, utilities, quality or manual work.
Minimum evidence set
Questions before specification
Answers are planning guidance. Project requirements and performance remain subject to confirmed data and agreements.
Not necessarily. Its stop may be a propagated response. Compare initiating events, repeated restrictions and their effect on accepted line-end output.
Only if the space is usable accumulation and the downstream equipment can clear it. Persistent capacity mismatch cannot be corrected by storage alone.
Look at repeated short stops, restart delay, utility fluctuation, reject losses and the time basis of the ratings. Sustained connected behavior can differ from isolated demonstrations.
Next buyer step