Production Performance Brief
How to Accept Water Bottling Line Output
Turn the production promise in a quotation into evidence that purchasing and engineering can check together at FAT and SAT.
Direct answer
What proves that a water bottling line meets its output requirement?
Review point 01
Separate the available factory test from the installed-line claim
A FAT can demonstrate the machines, connections and materials actually present at the factory. If the final packer, conveyors or site utilities are absent, identify the missing proof explicitly. SAT checks the installed combination; the name of the test alone does not establish what was demonstrated.
- Record included machines, retained equipment, simulated signals and temporary utilities.
- Identify checks that require final site materials or connections.
- Keep this output assessment separate from shipment release and the full project handover.
Review point 02
Fix the counting point and clock before the run
Write the required accepted quantity, test duration, bottle and final pack. As an illustration, 40,000 accepted bottles over an agreed 8-hour window means an average of 5,000 accepted bottles/h on that same window. A short burst above 5,000 does not establish the full-window result.
- State whether normal replenishment, planned changeovers and stops are included.
- Record the full elapsed window; disclose any exclusions agreed beforehand.
- If counting packs, count complete accepted packs and use the agreed bottles per pack.
Review point 03
Observe interruptions and recovery, not only steady running
A connected test should reveal whether upstream and downstream equipment recover under the agreed operating conditions. Log the initiating stop, propagated starved or blocked states, restart and return of accepted output. Overlapping machine stops are not separate elapsed line downtime.
- Use only approved test procedures carried out by qualified personnel; never bypass guards or safety functions.
- Record material replenishment, manual intervention and parameter changes.
- Preserve raw counter readings, timestamps and quality-disposition records.
Review point 04
Decide on evidence and identify the missing test
Compare the result with the requirement ID and its agreed criteria. Separate demonstrated, failed, not tested and conditional findings. A fast run with unacceptable packages is not accepted production. If an interface or material changes, assess which evidence must be repeated rather than simply reusing the old pass.
- Assign each deviation an owner, corrective action, evidence and retest condition.
- Keep an unresolved count discrepancy visible; do not balance it with an invented reject number.
- Send the production requirement and non-confidential test record to discuss the remaining performance question.
Prepare the output evidence before the test
Use the blank, editable text record for agreed inputs and raw observations. It sets no universal pass limit and is not a certificate or contractual acceptance.
Download blank output record (.txt)| Observed setup | Evidence it can provide | Still to verify |
|---|---|---|
| Isolated filler on a short trial | Filler behavior for the tested bottle and conditions | Connected packing, sustained accepted output and site interfaces |
| Connected factory trial with substitutions | Performance of the documented temporary configuration | Effects of final materials, utilities and any absent equipment |
| Installed connected test on the approved SKU | Output and recorded behavior during that agreed window | Untested SKUs, changed conditions and unresolved deviations |
Catalog equipment evidence
See the machines behind this production-line question.
These Allot Tech catalog references connect the technical explanation to physical equipment. Each caption identifies the capacity, interface or acceptance evidence to confirm.
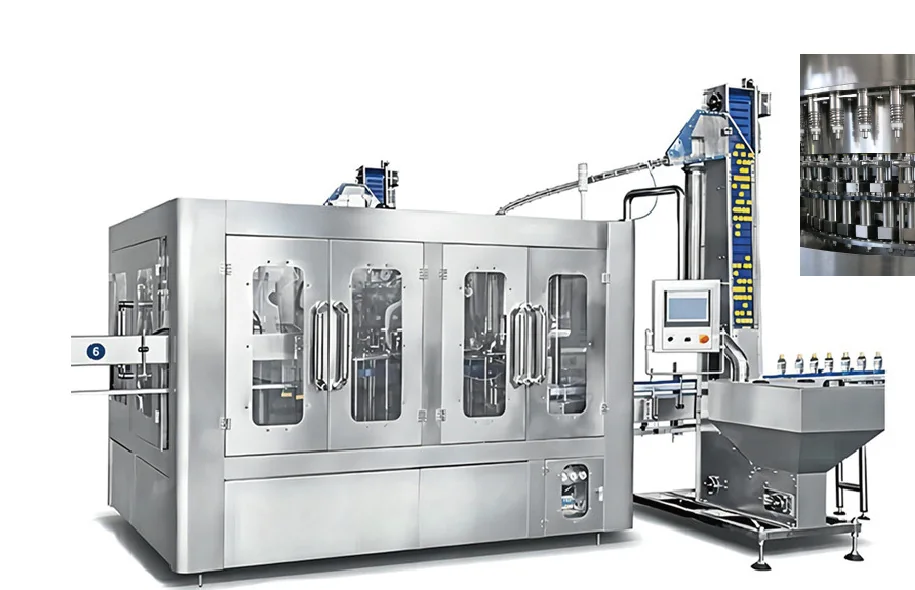
Rinse-fill-cap center
State filler BPH with the reference bottle, product, cap, test window and accepted-output counting point.
Review this interface basis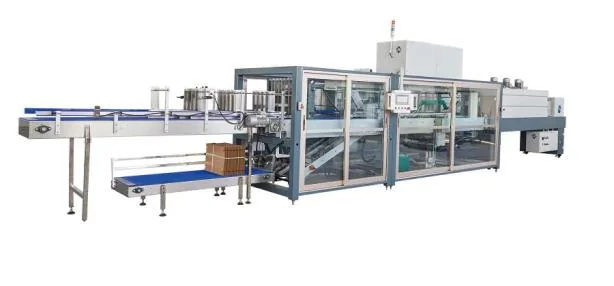
End-of-line packing system
The packer is one connected capacity node; pack pattern, cycle, bottle behavior and discharge flow set the usable rate.
Review this interface basisSource: Allot Tech Beverage Bottling Catalog 2026. Images are representative equipment references; final models and configurations remain project-specific.
Questions before specification
Frequently asked questions
Answers are planning guidance. Project requirements and performance remain subject to confirmed data and agreements.
Does a successful FAT prove installed shift output?
Only to the extent demonstrated by its documented connected scope, conditions and duration. Site-dependent checks and missing interfaces still require verification.
Is there one correct duration or efficiency percentage for every test?
No. Define them from the actual requirement and behavior to demonstrate before execution. This guide supplies no universal performance threshold.
Can bottles held for quality review count as accepted output?
Not while they remain unresolved under the agreed criteria. Record their disposition and counting boundary separately; do not count them both as accepted and held.
Next buyer step