Production Performance Brief
Bottling Line Performance Test Data Sheet
Make a production result reconstructible: another reviewer should be able to trace the quantity and time back to the same physical boundary.
Direct answer
How should bottling-line test counts be reconciled?
Review point 01
Define the record before filling in the result
Assign a test ID, protocol revision, requirement ID, SKU and equipment boundary. Identify each counter and its unit. Record start/end timestamps, time zone or clock basis, meter conditions, materials and who captured the observations. Keep raw exports beside the summary.
- Use final minus initial counter values; document resets, rollover or manual corrections.
- Convert complete packs to bottles only with the actual pack count.
- Do not merge readings from different clocks or unaligned windows.
Review point 02
Worked reconciliation: inventory changes the answer
Illustrative two-hour window: opening work-in-process is 300 bottles and 20,000 bottles enter the boundary. During the window, 19,700 accepted bottles leave, 150 rejects are removed, 50 held bottles are moved to quarantine outside the boundary, and 400 remain as closing work-in-process. Both sides equal 20,300.
- 300 + 20,000 = 19,700 + 150 + 50 + 400.
- Accepted rate: 19,700 ÷ 2 = 9,850 bottles/h, not the entry-counter rate of 10,000.
- The 50 quarantined bottles are excluded from closing work-in-process here; never count one physical group twice.
- These values illustrate record logic, not a customer result or equipment rating.
Review point 03
Keep events and quality disposition beside the counters
Record when a stop began, which machine initiated it, affected states, intervention and when accepted output resumed. Use mutually exclusive categories for accepted, rejected, quarantined and retained units. Where a movement or quality decision is unknown, leave an explicit unresolved item.
- Do not sum overlapping stops as separate line elapsed time.
- Show gross elapsed time and any pre-agreed excluded time separately.
- Retain evidence references for inspections and changes; a count sheet is not proof of product-water safety or regulatory compliance.
Review point 04
Close the evidence trail, not just the spreadsheet total
Recalculate the unit-count balance in the agreed unit and compare the result with the approved criteria. Record unexplained differences, their investigation and the required retest. A blank field or unsigned summary must not become an automatic pass.
- List result, evidence file, deviation owner and closure condition per requirement.
- Record preparer and authorized reviewers without treating the template as a sign-off.
- Redact confidential or personal details before sharing a planning copy with Allot Tech.
Download the blank count-and-time record
Editable UTF-8 text for your own agreed test. All measured fields are blank; no test is declared passed. Keep it with the raw evidence and approved protocol.
Download blank test data sheet (.txt)| Record group | Capture | Check before using the result |
|---|---|---|
| Identity and boundary | Test/protocol IDs, SKU, connected machines, count points | Same revision and production basis as the requirement |
| Time and counters | Start/end times and readings, units, resets, corrections | One aligned window; do not use a cumulative final value alone |
| Unit disposition | Opening/closing work-in-process, accepted exits, rejects, quarantined exits, other movements | No duplicate classification; explain any balance residual |
| Events and decision | Stops, recovery, interventions, evidence references and deviations | No missing data presented as passed evidence |
Catalog equipment evidence
See the machines behind this production-line question.
These Allot Tech catalog references connect the technical explanation to physical equipment. Each caption identifies the capacity, interface or acceptance evidence to confirm.

Water bottling production process flow
Separate water preparation, bottle supply, filling, decoration and packing, then compare every node on one output basis.
Review this interface basis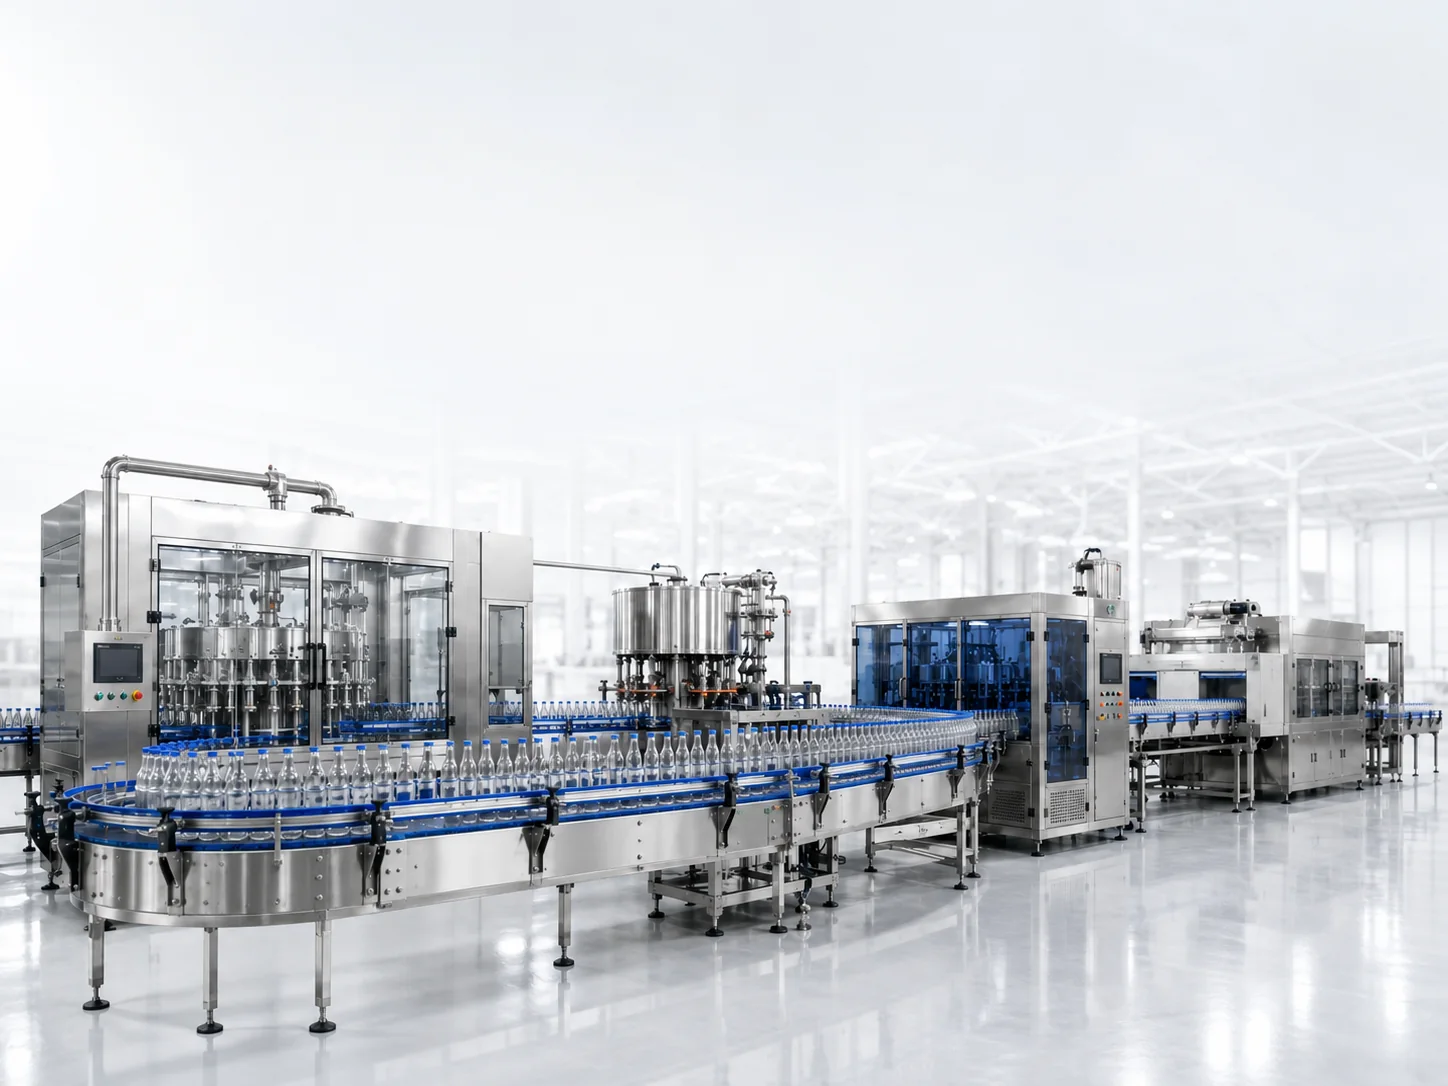
Connected water bottling line
Use the complete-line view to mark machine boundaries, transfer points, utilities, controls and output counting locations.
Review this interface basisSource: Allot Tech Beverage Bottling Catalog 2026. Images are representative equipment references; final models and configurations remain project-specific.
Questions before specification
Frequently asked questions
Answers are planning guidance. Project requirements and performance remain subject to confirmed data and agreements.
Why can the filler and packer counters disagree?
Their physical boundaries, start/finish times, rejects, pack units or retained inventory may differ. Align them and document movements before assigning the difference to loss.
Does a balanced count prove performance acceptance?
No. It makes the count reconstructible. The result must still meet the agreed scope, elapsed-time, output and quality criteria.
Can I send the text template through the website attachment field?
The form accepts PDF and supported images, not TXT. Paste a short non-confidential summary into the message or export your completed record to an accepted format.
Next buyer step