Production Performance Brief
Air Conveyor Accumulation for PET Water Bottles
Air-conveyor length becomes useful accumulation only when bottle geometry, rail settings, airflow, zoning and control logic support controlled recovery.
Direct answer
How much air-conveyor accumulation is actually usable?
Review point 01
Operating decision for Air Conveyor Accumulation for PET Water Bottles
Define accumulation by recoverable bottle time at the reference SKU, then verify it with controlled upstream and downstream stops.
- Bottle neck and body geometry
- Blower and filler sustained rates
- Expected short-stop durations
- Available conveyor route and access
Review point 02
Inputs and connected interfaces
Freeze the project inputs before comparing equipment or changing settings. The review must show where the decision connects to upstream supply, downstream demand, controls and utilities.
- Blower discharge spacing
- Air-conveyor zone controls
- Filler infeed pressure and gating
- Starved, blocked and speed-reference signals
Review point 03
Trade-offs and failure modes
A project-specific choice may improve one condition while moving risk to another node. Review these possible failure modes against the approved bottle, pack, operating window and installed conditions.
- Nominal conveyor length treated as usable buffer
- Bottle pressure produces scuffing or deformation
- Incorrect rail setup causes neck instability
- Restart releases bottles faster than the infeed can accept
Review point 04
Evidence and acceptance record
Close the decision with measurements and revision-controlled records. Final performance remains subject to the approved materials, equipment, utilities, operating conditions and agreed test procedure.
- Bottle-count or occupancy test by zone
- Controlled stop and release video
- Rail and airflow setting record
- Filler starvation log before and after adjustment
Catalog equipment evidence
See the machines behind this production-line question.
These Allot Tech catalog references connect the technical explanation to physical equipment. Each caption identifies the capacity, interface or acceptance evidence to confirm.
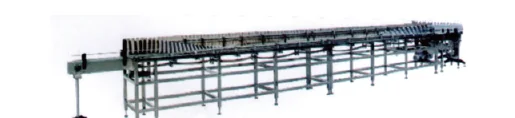
Air conveyor and bottle accumulation
Usable accumulation is a controlled time buffer, not simply conveyor length. Confirm bottle stability and recovery after stops.
Review this interface basisSource: Allot Tech Beverage Bottling Catalog 2026. Images are representative equipment references; final models and configurations remain project-specific.
Questions before specification
Frequently asked questions
Answers are planning guidance. Project requirements and performance remain subject to confirmed data and agreements.
What information should a buyer send for Air Conveyor Accumulation for PET Water Bottles?
Send the confirmed project inputs, drawings, current line records, photos or video where relevant, and keep unknown values clearly marked for project review.
Does this guide guarantee a production result?
No. It provides a structured planning and evidence basis. Final configuration and performance require project-specific confirmation and an agreed acceptance procedure.
Next buyer step